1
/
of
6
flexiblediamondabrasive
6" x 1.5" 280 Grit Diamond Hard Flat Grinding Wheel for Hard Materials
6" x 1.5" 280 Grit Diamond Hard Flat Grinding Wheel for Hard Materials
Regular price
$55.56 USD
Regular price
Sale price
$55.56 USD
Taxes included.
Shipping calculated at checkout.
Quantity
Couldn't load pickup availability
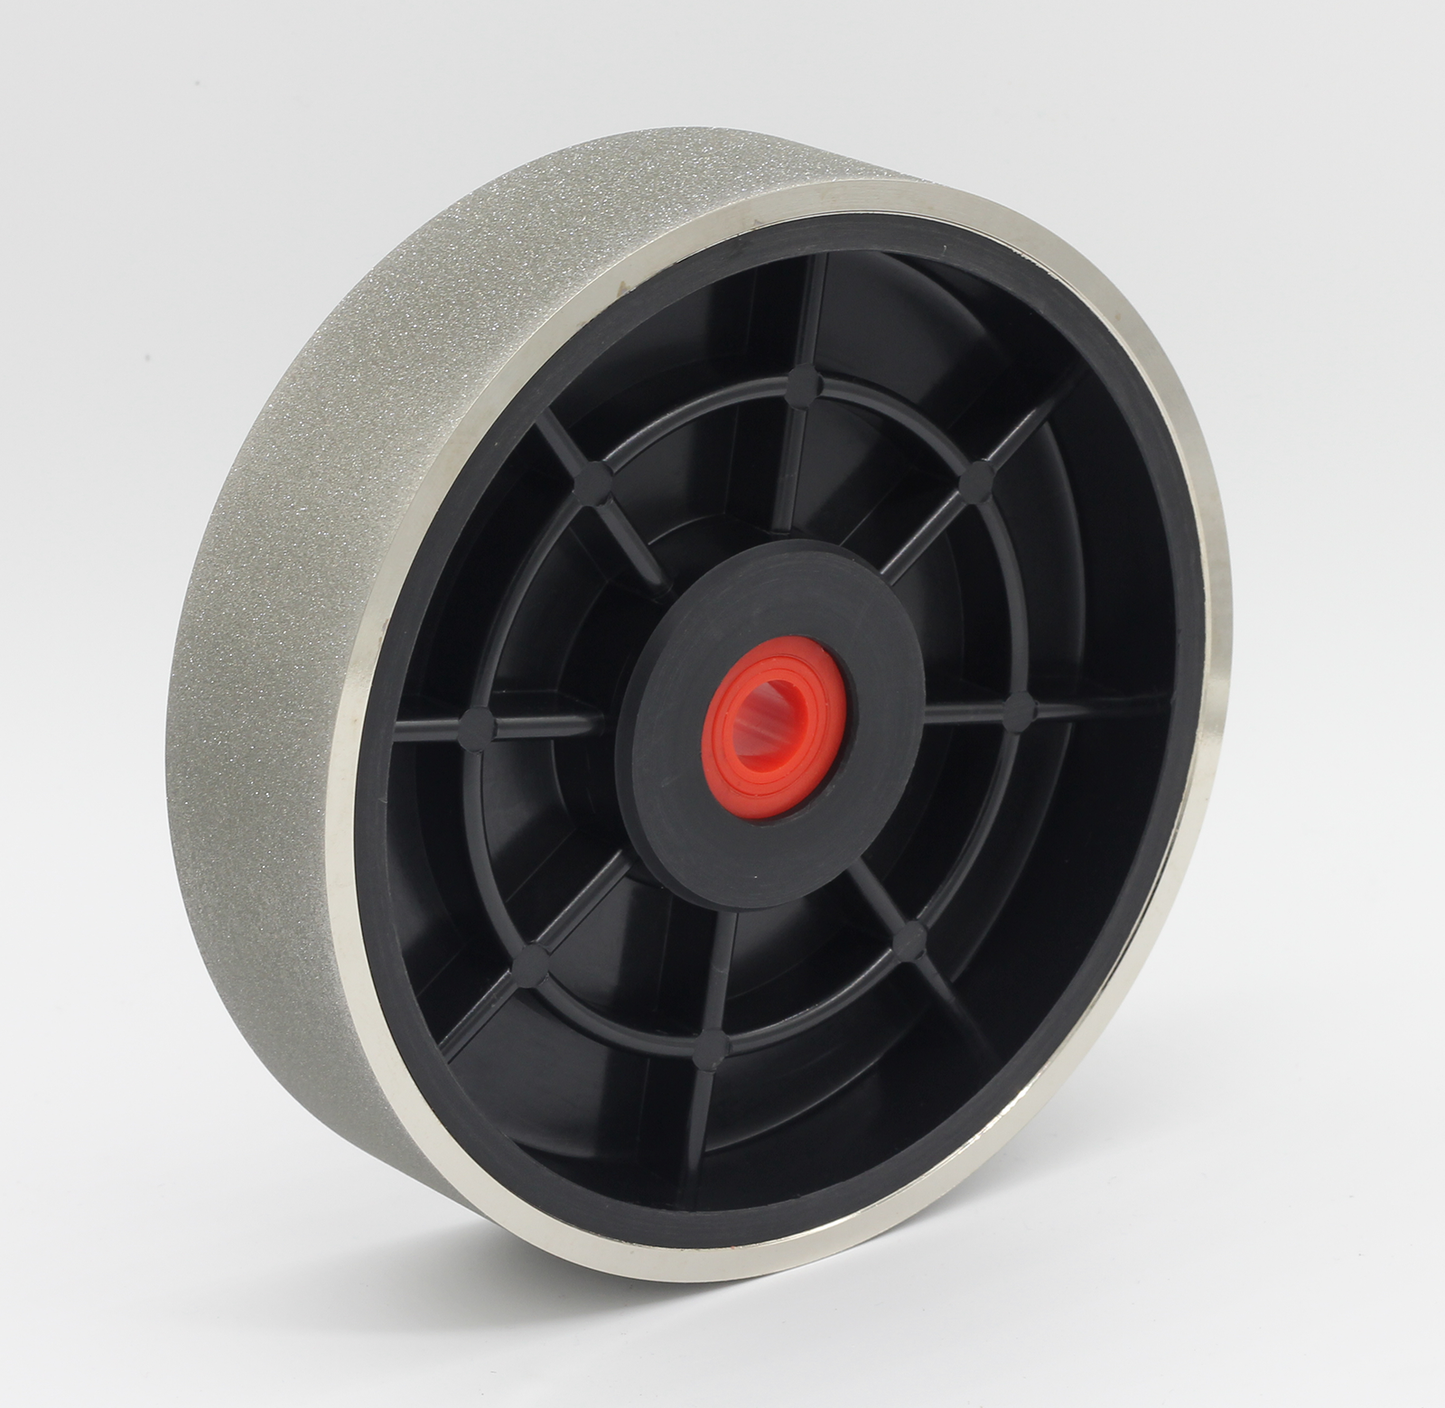
The 6" x 1.5" 280 Grit Diamond Hard Flat Grinding Wheel is manufactured with a seamless solid steel core and a high-precision electroplated diamond rim. Specially designed for smooth fine shaping, pre-polishing scratch elimination, and refined contouring on hard materials such as gemstones, rocks, glass, ceramics, and porcelain. Delivers true concentric rotation and vibration-free grinding on standard lapidary machines.
Key Features
- Solid Seamless Steel Core: Heavy-duty steel body ensures true-running concentricity and eliminates wheel vibration.
- Precision Electroplated Diamond Rim: Uniform 280-grit diamond plating bridges the gap between coarse roughing and resin fine polishing.
- True Flat Profile: Perfectly flat grinding face prevents dishing or crowning during shaping and faceting pre-forming.
- Universal 1" Arbor: Standard 1-inch inner bore fits standard lapidary cabbing machines (compatible with 3/4", 5/8", and 1/2" reducer bushings).
Applications
- Lapidary & Gemstones: Fine pre-polishing and scratch removal on agate, jasper, quartz, jade, and petrified wood cabochons.
- Glass Cold Working: Fine edge smoothing, seaming, and scratch blending on decorative glass and optical components.
- Ceramic & Porcelain: Precision smoothing and surface refining of technical ceramics and mineral specimens.
Technical Specifications
- Diameter: 6 inches (150 mm)
- Width: 1.5 inches (38 mm)
- Grit: 280 Grit (Fine Grinding / Pre-Polishing Smoothing)
- Bond Type: Electroplated Diamond
- Core Material: Solid Steel
- Arbor Size: 1 inch (compatible with reducer bushings)
- Recommended Operating Speed: 1725–1800 RPM
Operating Guidelines
- Continuous Water Coolant Required: Always operate with adequate water flow to flush grinding swarf and keep diamond particles cool.
- Apply light, consistent workpiece pressure across the wheel face to prevent localized grooving.
Share